
A modern rocket engine used to be an argument between thousands of parts. GE’s additively manufactured LEAP fuel nozzle famously collapsed twenty brazed and welded components into one printed piece — 25% lighter and roughly five times more durable — and more than one hundred thousand of them have since flown on commercial aircraft. Rocket builders went further: SpaceX printed SuperDraco combustion chambers in Inconel a decade ago, Rocket Lab’s Rutherford engine prints its primary components, and NASA has printed and hot-fire tested aluminum rocket nozzles and new superalloys that hold their strength above 1,000 °C. Additive manufacturing is no longer a curiosity in aerospace. It is how the most demanding hardware in the industry increasingly gets made.
But printing a part is the easy half of the problem. The hard half is knowing the part is good — proving that a component grown from powder, layer by layer, thousands of laser passes deep, contains no hidden flaw that will matter at 300 bar chamber pressure or after ten years in vacuum. That is a data problem as much as a materials problem. And it is exactly where Space Dust Industries is placing its bet: applying serious AI to the full life of a printed part — its design, its build, its inspection, and its paper trail.
How Metal Printing Actually Works
The workhorse of aerospace metal AM is laser powder bed fusion (LPBF, often called DMLS). A recoater spreads a layer of metal powder 20–60 microns thick — thinner than a human hair — and a high-power laser selectively melts the cross-section of the part into the layer below. The bed drops, powder spreads again, and the part grows: a single component can be tens of thousands of layers and days of continuous melting. Titanium alloys, Inconel and other nickel superalloys, aluminum, copper alloys, and stainless steels are all routinely processed this way, in an inert or near-vacuum atmosphere that keeps reactive metals from oxidizing mid-build. The payoff is geometry: conformal cooling channels inside a combustion chamber wall, lattice cores, internal passages no drill could ever reach — with material densities above 99.5% of theoretical.
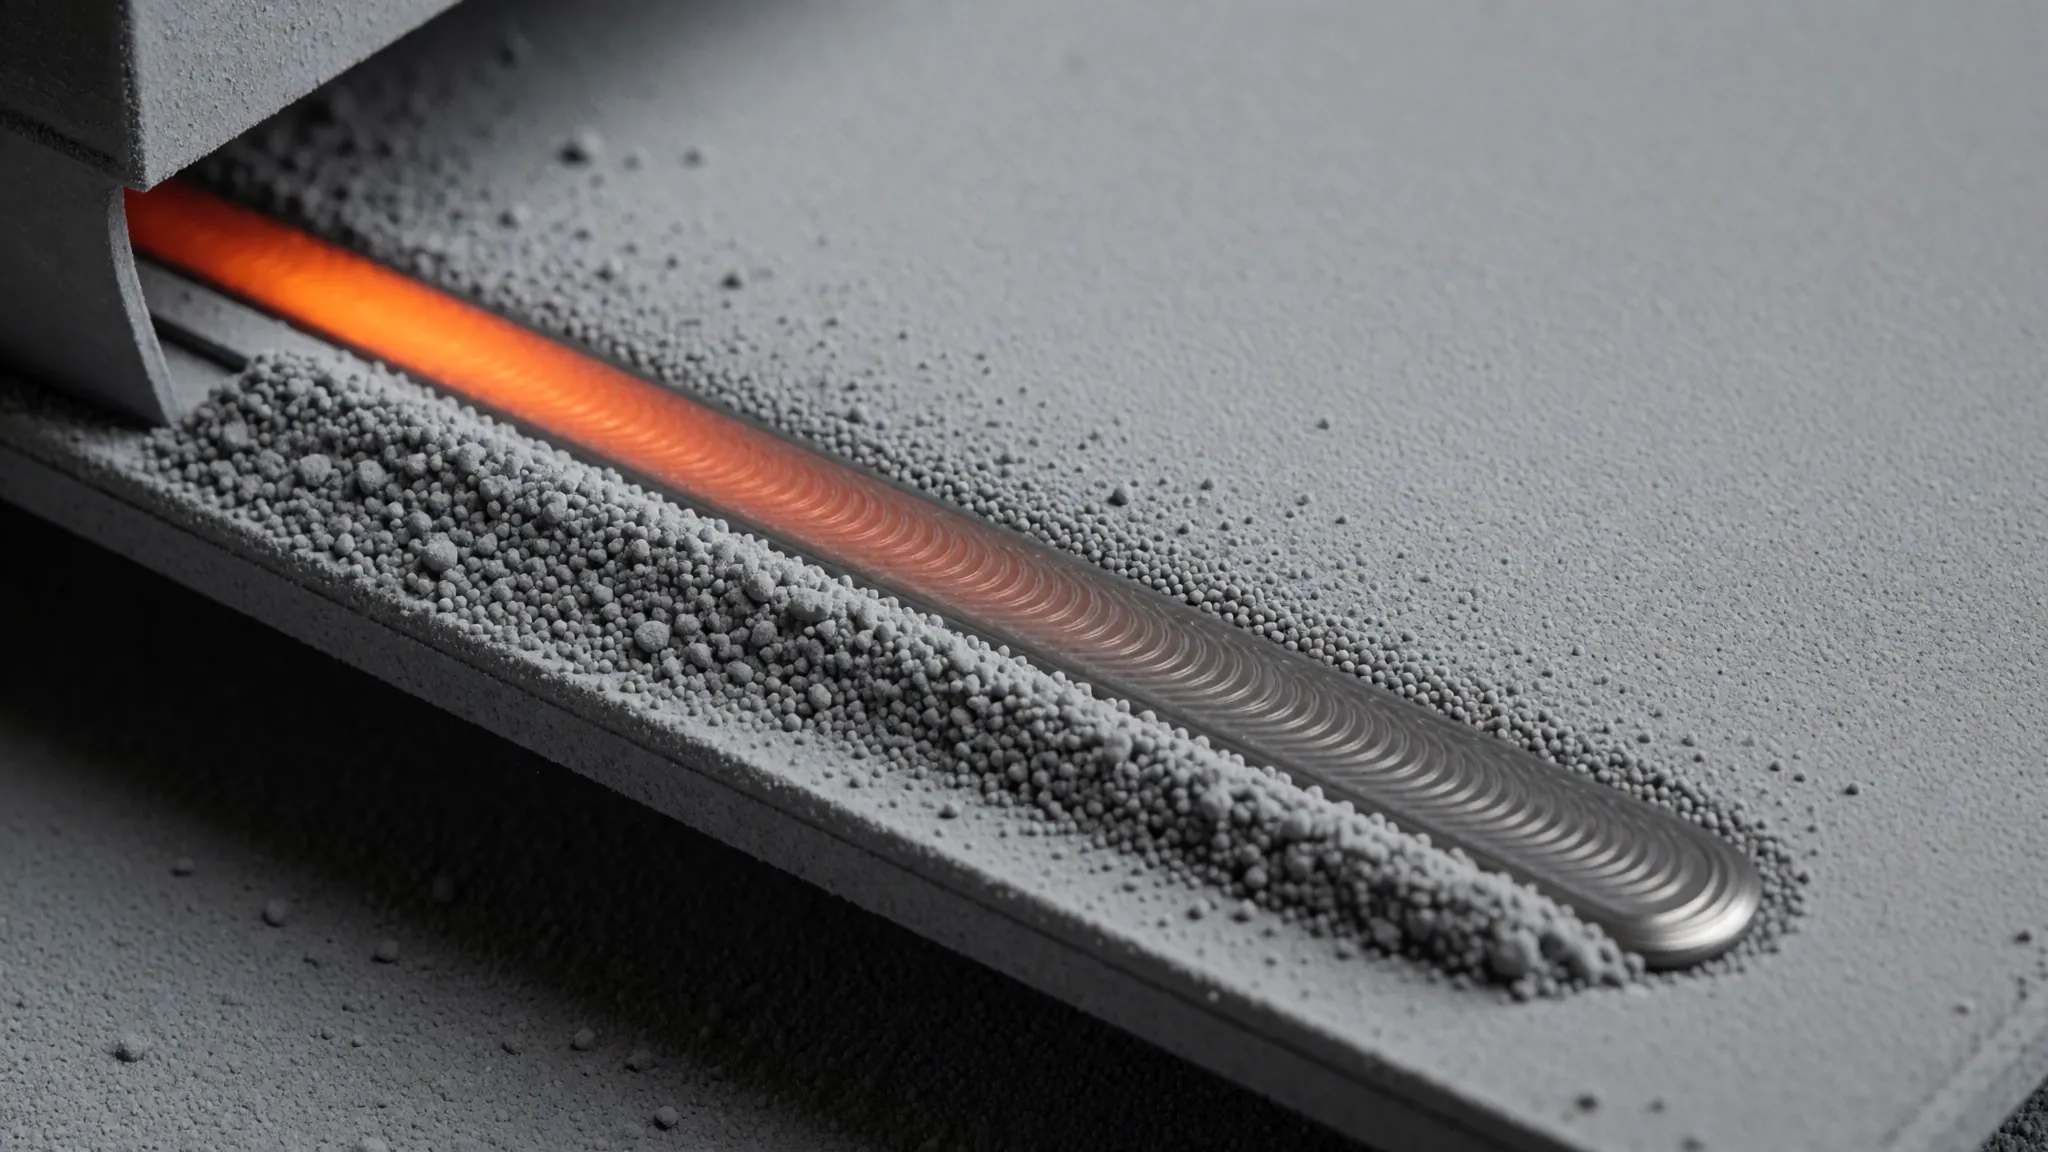 Powder bed fusion in a controlled atmosphere: a laser fuses metal powder in layers measured in tens of microns.
LPBF is not the only tool. Electron beam melting works in hard vacuum at elevated temperatures, which suits crack-prone alloys. Directed energy deposition feeds wire or powder into a melt pool to build or repair large structures at high deposition rates. And cold spray — a process we have long studied for nozzle fabrication and repair — takes a different path entirely: metal particles accelerated through a supersonic nozzle to hundreds of meters per second bond on impact, in solid state, below their melting point. No melt pool means no heat-affected zone, which makes cold spray uniquely attractive for repairing flight hardware without cooking the metallurgy around the repair. Our research treats these as a portfolio, not competitors: each process has a physics regime where it wins.
Watching the Melt Pool: AI as the Inspector
Here is the uncomfortable truth of powder bed fusion: the melt pool — the tiny puddle of liquid metal under the laser — is on the order of 100 microns wide and cools at rates approaching a million degrees per second. Porosity, keyholing, lack-of-fusion, spatter: the defects that kill parts are born in milliseconds, buried under the next layer, and invisible from the outside. Traditional quality control answers this with after-the-fact CT scanning and destructive testing of witness specimens — expensive, slow, and statistical rather than certain.
The state of the art is moving inside the machine. Modern systems watch every laser pass with coaxial photodiodes, high-speed cameras, and thermal imaging, generating enormous streams of melt-pool data per build. The signal is there — melt-pool brightness, shape, and thermal history correlate with porosity that later shows up in CT — but no human can read millions of sensor samples per part. Machine learning can. Models trained to link in-situ sensor signatures against CT-verified ground truth are beginning to flag defective layers as they happen, turning quality control from an autopsy into a diagnosis.
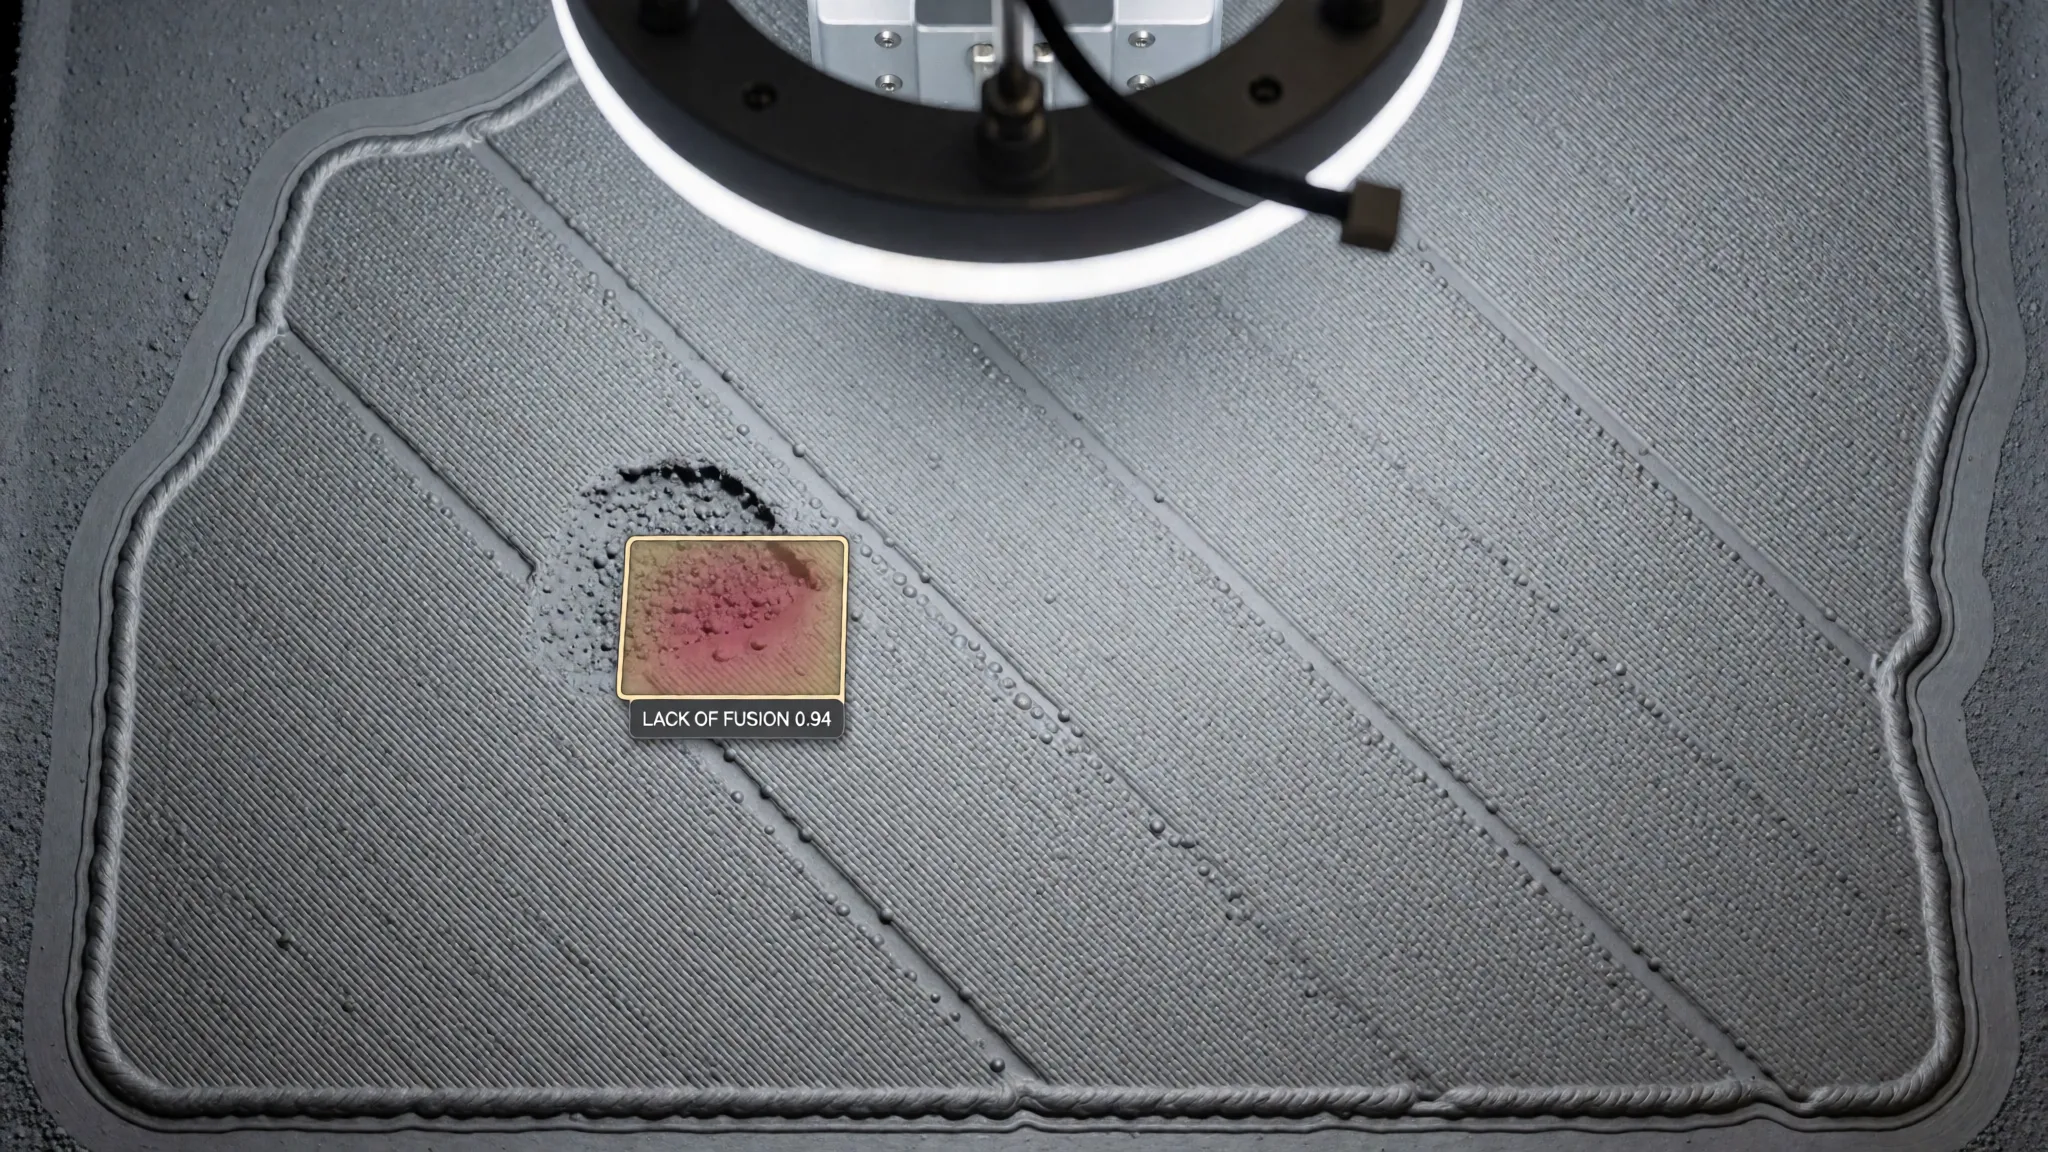 Layer-wise imaging plus machine learning: defect signatures caught during the build, not discovered after it.
This is SDI’s home turf. Our team builds and trains vision and anomaly-detection models on our own on-premises multi-GPU cluster, and our research concentrates on the fusion problem — combining layer-wise optical inspection (the AOI playbook proven in electronics manufacturing), thermal imagery, and machine telemetry into a single per-part record a model can reason over. The goal is not a prettier dashboard. It is a printed part that arrives with evidence: a complete, machine-analyzed history of every layer it is made of.
Designing Parts No Human Would Draw
Additive manufacturing removes most of the constraints that shaped a century of mechanical design — and generative design tools exploit that freedom. Give an algorithm the loads, the keep-out zones, the material, and the manufacturing process, and it evolves structures that look grown rather than machined: branching, organic, and startlingly efficient. NASA Goddard’s “evolved structures” work has cut the mass of individual spacecraft brackets by as much as two-thirds, with candidate designs generated in about an hour instead of days; hardware from that program flew on the EXCITE exoplanet telescope balloon mission launched in 2024. Commercial tools from Autodesk, nTop, and others have pushed the same approach across the aerospace industry, with printed, topology-optimized parts routinely landing 30–60% lighter than their conventional ancestors.
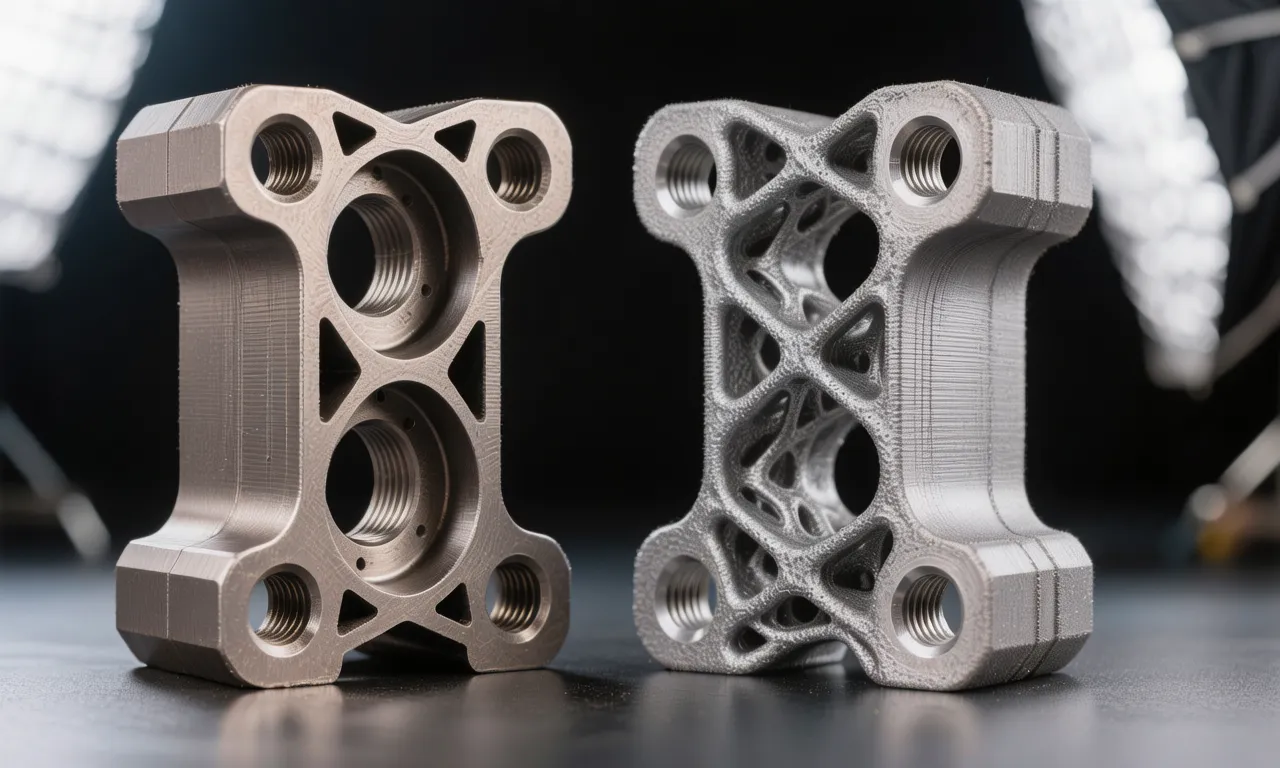 Generative design explores thousands of load-bearing geometries a human would never sketch — and additive manufacturing is the only way to build most of them.
For a launch customer, every kilogram removed is money; for a deep-space mission, it is margin. Our work connects this front end to the back end: designs generated with the printer’s physics in mind — overhang limits, thermal behavior, inspectability — so that “optimized” also means buildable and provable. A brilliant geometry that cannot be inspected is not flight hardware.
Manufacturing Off the Planet
The case for making things in space is brutal logistics: every spare part launched is mass stolen from the mission, and no supply chain reaches an outbound spacecraft. The milestones are real and recent. Made In Space (now Redwire) printed the first part manufactured off Earth aboard the ISS in 2014, and its successor facility has been turning out polymer tools and components on-orbit ever since. Redwire’s Archinaut program demonstrated 3D printing of multi-meter structural beams under space-like thermal vacuum conditions on the ground. And in 2024, an ESA/Airbus technology demonstrator became the first metal printer in space: installed in the ISS Columbus module, sealed into a nitrogen-purged safety enclosure, it deposited stainless steel layer by layer with a laser and delivered its first finished specimens back for analysis that August.
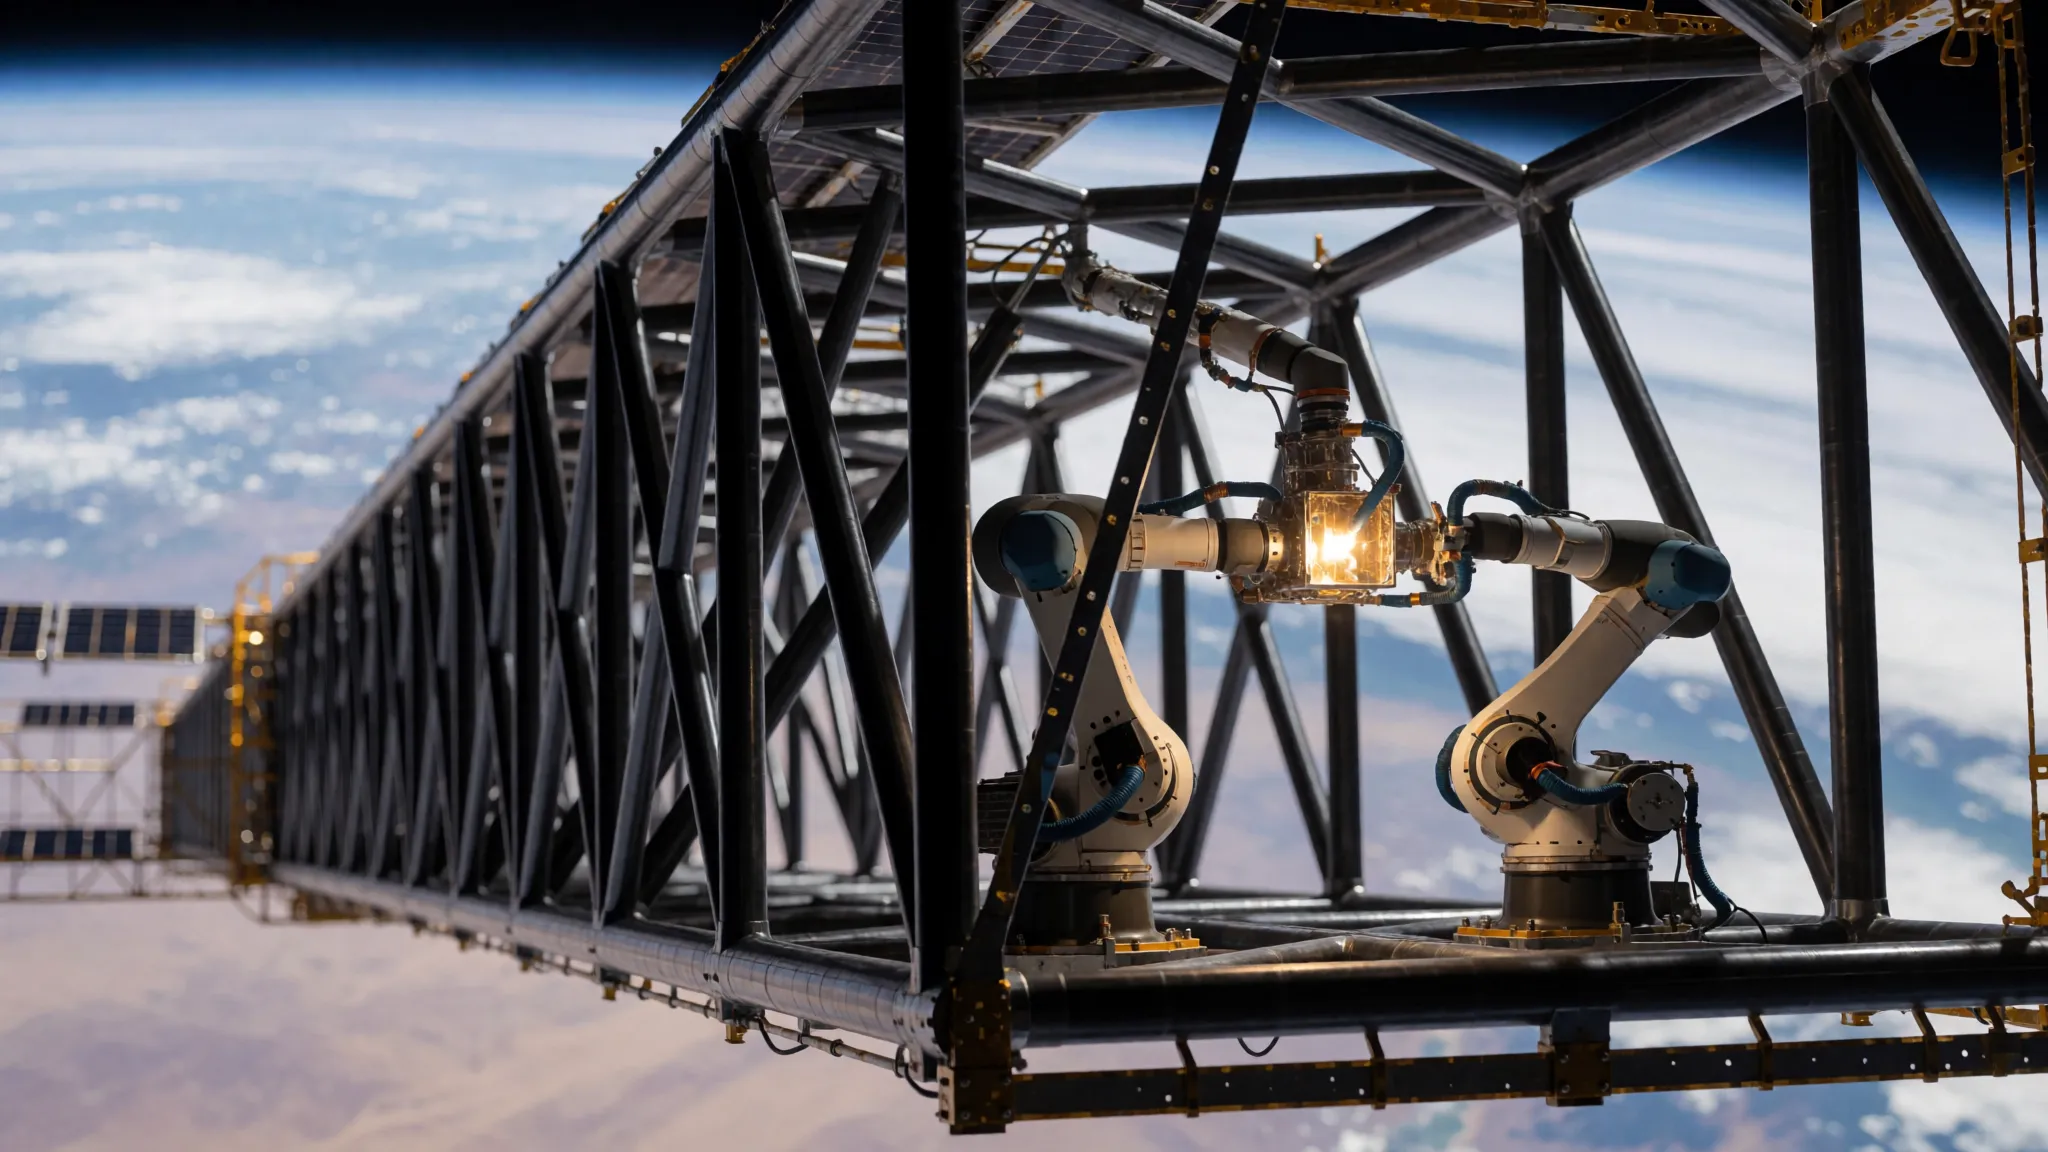 On-demand fabrication in orbit: the endgame is structures built where they are needed, sized by physics rather than by payload fairings.
Space changes the process in ways engineers are still mapping. Loose powder is nearly unmanageable in microgravity, which is why orbital metal printing leans toward wire-fed and deposition-based approaches. Without gravity there is no buoyancy-driven convection in the melt, altering how heat and solidification behave. Vacuum removes oxidation but also removes convective cooling — heat leaves only by radiation and conduction. And nobody is standing next to the machine: an orbital factory must run itself, monitor itself, and judge its own output. That last requirement is why we believe in-space manufacturing is ultimately an autonomy problem — and why the AI quality-control stack we are developing on the ground is the same technology an orbital printer will need to be trusted without a human inspector in the room.
The Trust Problem
The gap between a printed part and a flight part is qualification. NASA’s NASA-STD-6030 (built on Marshall’s pioneering MSFC-STD-3716) defines how additively manufactured spaceflight hardware is classified by risk and controlled from powder to final inspection; SAE’s AMS7000-series specifications do the same for the broader aerospace industry, locking down materials and process parameters for repeatable production. The common thread through all of them is process history: qualification lives or dies on documented evidence that every step — powder lot, machine state, build parameters, inspection results — was controlled and recorded. Today that evidence trail is largely assembled by hand, and it is one of the biggest cost and schedule burdens in flight-qualified AM. It is also, unmistakably, a job for machines that read, correlate, and never lose a record.
The Road Ahead
SDI has not flown hardware, and we say so plainly. What we are building today is the foundation this whole field converges on: AI that understands manufacturing data. On the ground, our near-term direction is a metal additive manufacturing service for exotic aerospace alloys, wrapped in an AI-driven documentation and quality stack — the melt-pool analytics, automated inspection, and qualification-grade traceability described above, running on our own GPU infrastructure and paired with the 3D scan-to-print pipeline we operate now. Every model we train on terrestrial build data, every defect our systems learn to catch, is a step toward the same systems judging a build in a place no inspector can go. The path to manufacturing in orbit runs through proving, on Earth, that a machine’s word about a part can be trusted. That proof is what we are engineering.